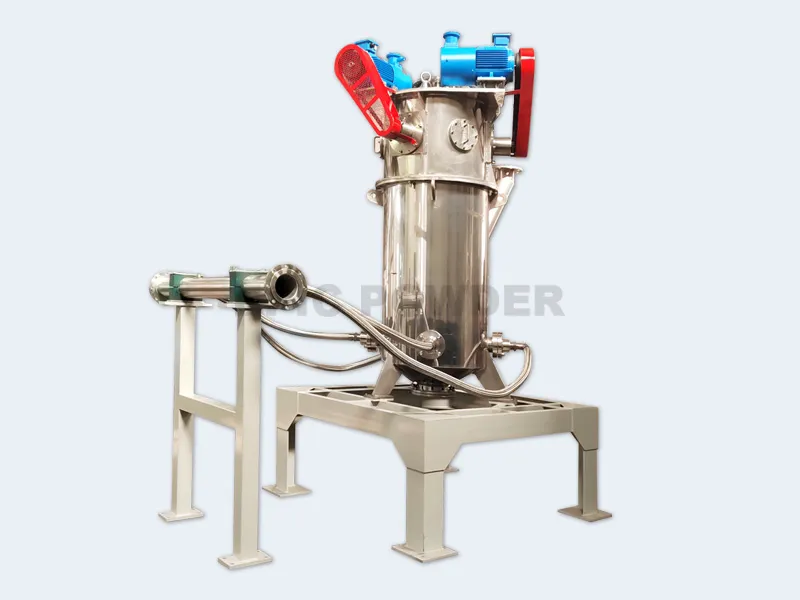
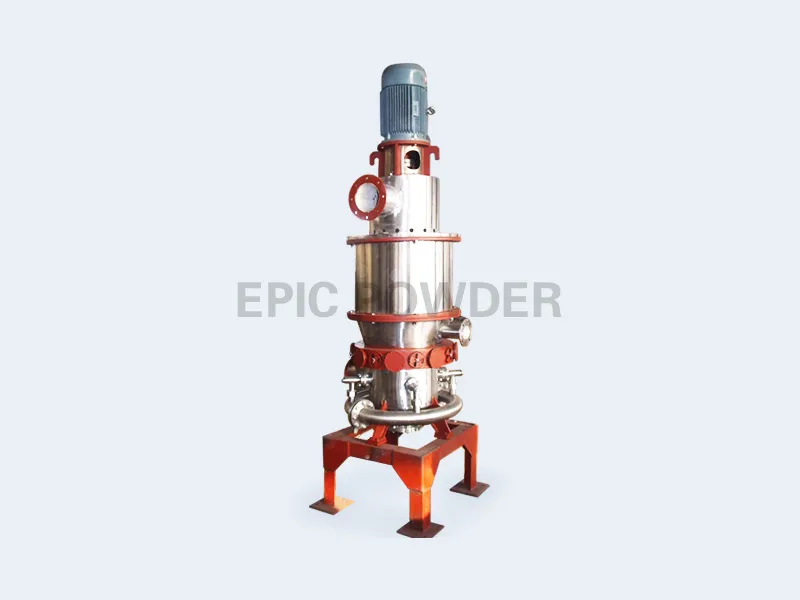
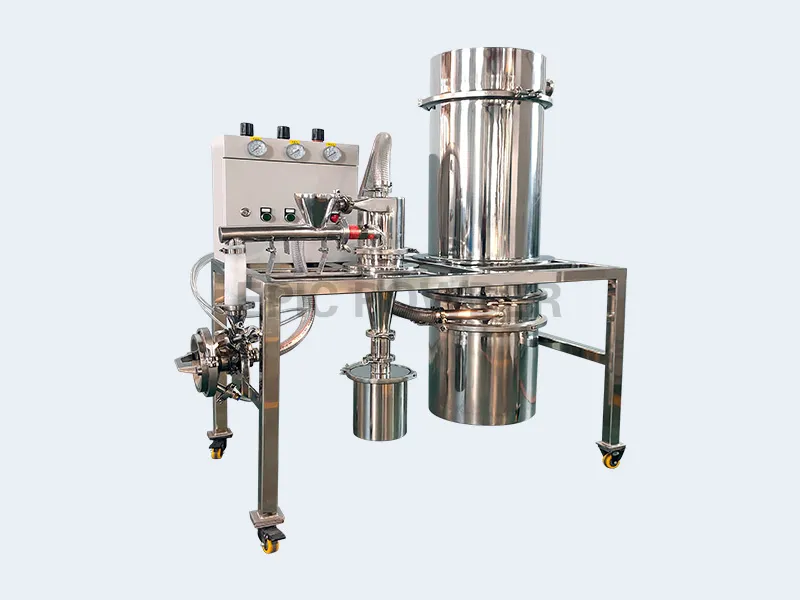
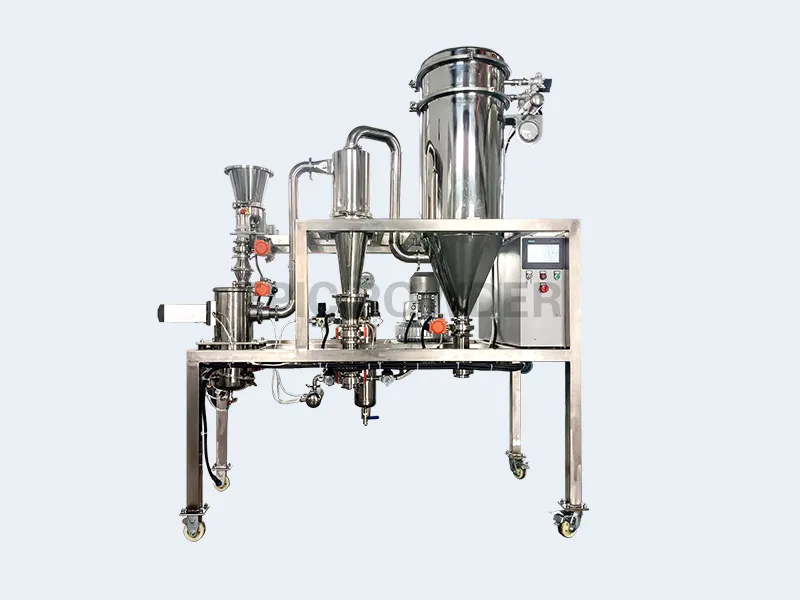
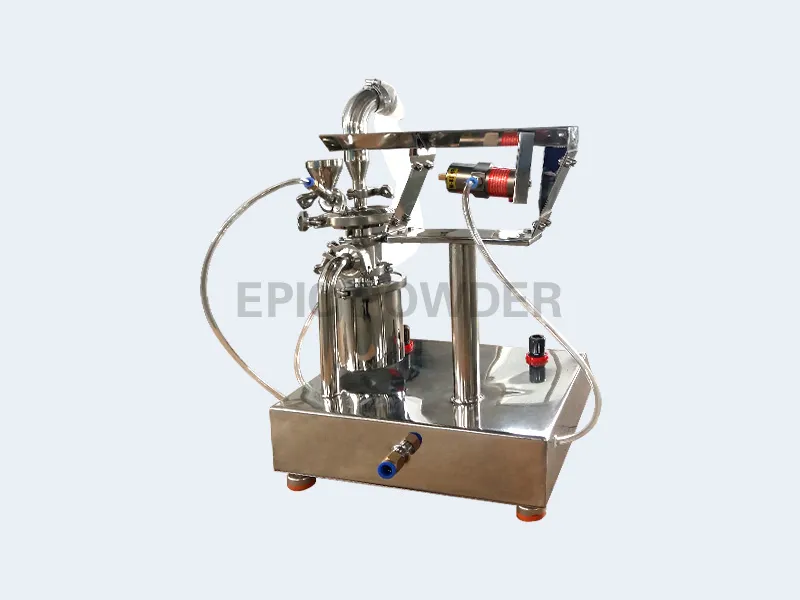
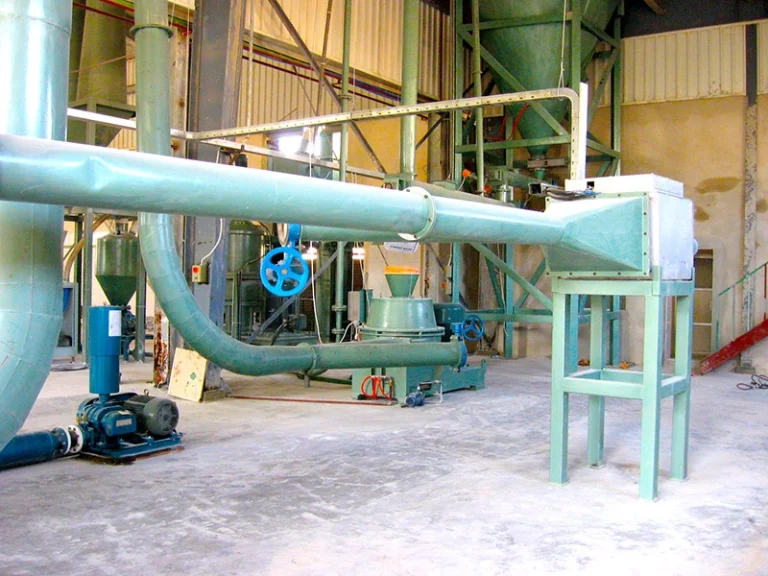
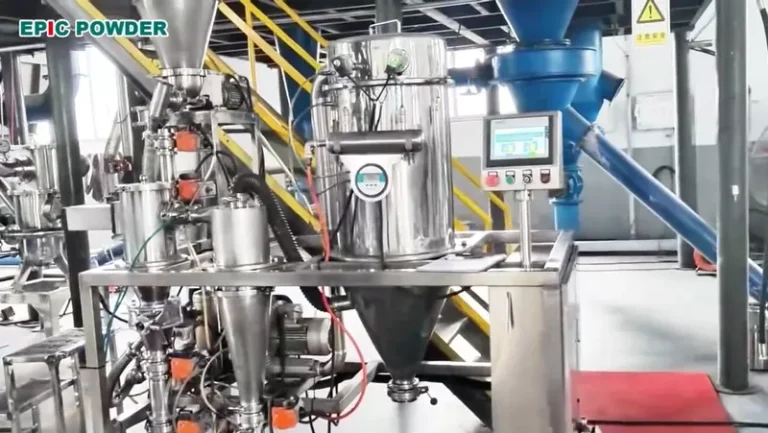
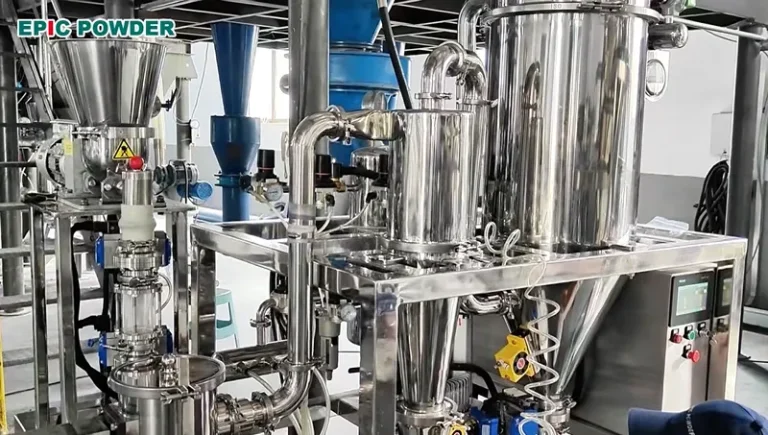
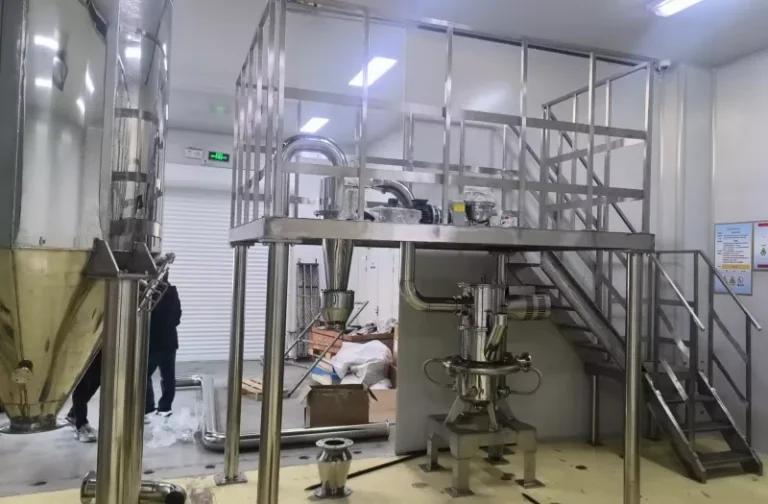
โรงสีเจ็ท MQW เป็นโรงสีเจ็ทตรงข้ามฟลูอิดไดซ์เบด ซึ่งมีล้อแยกประเภทแนวนอนในตัว (ล้อเดียวหรือหลายล้อ) หลังจากที่อากาศอัดถูกกรองและทำให้แห้งแล้ว ก็จะถูกพ่นเข้าไปในห้องบดผ่านหัวฉีด Laval ด้วยความเร็วสูง ที่จุดตัดของกระแสลมแรงดันสูงหลายจุด วัสดุจะถูกชนกัน ถู และตัดซ้ำหลายครั้งเพื่อบดขยี้ วัสดุพื้นจะเพิ่มขึ้นตามแรงดูดของพัดลม การไหลของอากาศเคลื่อนไปยังพื้นที่จำแนกประเภท ภายใต้แรงเหวี่ยงที่แข็งแกร่งซึ่งเกิดจากกังหันจำแนกประเภทหมุนด้วยความเร็วสูง วัสดุหยาบและละเอียดจะถูกแยกออก อนุภาคละเอียดที่ตรงตามข้อกำหนดขนาดอนุภาคจะเข้าสู่ตัวแยกพายุไซโคลนและตัวเก็บฝุ่นผ่านการจำแนกประเภท ล้อและอนุภาคหยาบลงไปที่บริเวณการเจียรเพื่อทำการเจียรต่อไป
โรงบดอัดอากาศแบบฟลูอิดไดซ์เบด: หลังจากกรองและทำให้แห้งแล้ว อากาศอัดจะถูกพ่นเข้าไปในห้องบดด้วยความเร็วสูงผ่านหัวฉีด Laval ที่จุดตัดของกระแสลมแรงดันสูงหลายจุด วัสดุจะถูกชนกัน ถู และตัดซ้ำหลายครั้งเพื่อบดขยี้ วัสดุที่ถูกบดจะลอยขึ้นตามการดูดของพัดลม กระแสลมจะเคลื่อนไปยังโซนการจำแนกประเภท ภายใต้การกระทำของแรงเหวี่ยงหนีศูนย์ที่แข็งแกร่งซึ่งเกิดจากกังหันจำแนกประเภทหมุนด้วยความเร็วสูง วัสดุหยาบและละเอียดจะถูกแยกออกจากกัน อนุภาคละเอียดที่ตรงตามข้อกำหนดขนาดอนุภาคจะเข้าสู่เครื่องแยกพายุไซโคลนและตัวเก็บฝุ่นผ่านวงล้อจำแนกเพื่อรวบรวม และอนุภาคหยาบจะลงไปที่บริเวณการบดและยังคงถูกบดขยี้ต่อไป
| พารามิเตอร์/ รุ่น | MQW03 | MQW06 | MQW010 | MQW20 | MQW30 | MQW40 | MQW60 | MQW80 | MQW120 | MQW160 | MQW240 |
|---|---|---|---|---|---|---|---|---|---|---|---|
| ขนาดการป้อน (มม.) | <1 | <2 | <2 | <3 | <3 | <3 | <3 | <3 | <1 | <3 | <3 |
| กำลังการผลิต (กก./ชม.) | 0.3~10 | 10~150 | 20~300 | 40~600 | 100~900 | 200~1200 | 500~2000 | 800~3000 | 1500~6000 | 2000~8000 | 4000~12000 |
| ขนาดอนุภาค (D97:μm) | 3~45 | 3~45 | 3~45 | 3~45 | 3~45 | 3~45 | 3~45 | 3~25 | 15x4 | 15x6 | 15x6 |
| มอเตอร์ตัวแยก (กิโลวัตต์) | 2.2 | 3 | 5.5/7.5 | 7.5/11 | 11/15 | 15/7.5x3 | 7.5x3 | 11x3 | 15x3 | 15x4 | 15x6 |
| ปริมาณการใช้อากาศ (ลบ.ม./นาที) | 3 | 6 | 10 | 20 | 30 | 40 | 60 | 80 | 120 | 160 | 240 |
| ความดันอากาศ (Mpa) | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 | 0.6~1 |
หมายเหตุ: กำลังการผลิตมีความสัมพันธ์อย่างใกล้ชิดกับขนาดอนุภาค ความถ่วงจำเพาะ ความแข็ง ความชื้น และตัวชี้วัดอื่นๆ ของวัตถุดิบ ข้อมูลข้างต้นใช้สำหรับการอ้างอิงการเลือกเท่านั้น
Among particle size reduction technologies, jet milling’s advantages include:
It can achieve very fine particles. It also creates tight size distributions. This is better than other milling methods.
No knives, blades, or hammers. Also, no milling media or screens. This means minimal risk of contamination from worn mill parts.
The simple chamber design is easy to clean, reducing risk of cross contamination
Grinding doesn’t cause temperature changes. This is unlike mechanical mills. Such changes are important for heat-sensitive materials.
Different materials act differently on the jet mill. The best materials are:
Abrasive
Brittle
Dense
Hard
Very friable (in other words, easy to crumble)
Jet mills also have their disadvantages, though they’re few. For one, they can be expensive to buy — which is why working with a toll processor is a smart business decision. A partnership can be a great way to get the benefits of jet milling technology and still manage costs. The process also needs high energy. It needs specialty gases and other special items to meet the specs.
Materials that may respond poorly to the jet milling process are often:
Elastic
Wet
Sticky
Light and fluffy
Easily deformed
Shock absorbent
Difficult to accelerate
Of course, a toll processor has years of experience. They have been meeting tough particle specs. They already have the gear and know-how. They can use it well to get the best results.
By working with a tolling partner’s technical team, you will gain efficiency. They will help choose the best mill type. They will also pick the right speed and feed rate. They will also cover any special project needs.
The team brings focused insights and extensive experience to the table. However, you should also expect to provide safety data sheets and answer a few questions, such as:
A jet mill is a type of ultrafine grinding equipment. It is a machine that uses a lot of energy. Therefore, the feed particle size of the air flow mill should be as fine as possible. It is recommended that the feed particle size be less than 80 mesh. Under normal circumstances, the feed particle size needs to be less than 1 mm.
Jet milling usually makes particles that are 1 to 10 microns in size. This is referred to as micronization.
Some product formulations require particles as small as 200 nanometers. The material's properties determine how small these sizes can be. You can make them smaller by increasing the mill's power. Additionally, by increasing the time the material spends in the milling chamber.
Some products require particles larger than 10 microns. This can be achieved by reducing the power to the mill or increasing the feed rate to the equipment.
In both circular and fluidized bed mills, jets of air or steam are made by gas. The gas is compressed to a gauge pressure of 50 to 120 psig. The most common gas used is commercially compressed air.
Superheated steam (392–980°F) is compressed to 100–220 psig. It can also be used on raw feed materials that are not heat-sensitive. Some of the other gases used include:
Nitrogen, which can protect materials from oxidation and/or fire
Argon, another inert option, though more expensive than nitrogen
Helium, used to achieve higher-velocity impact between particles
A great deal of energy is needed to create enough momentum to cause particles to break on impact. The compressor and nozzles turn high air pressure into energy. They do this within the mill. Large particles recirculate, and multiple high-velocity collisions progressively reduce their mass.
ติดต่อเราทาง WhatsApp
กรุณากรอกแบบฟอร์มด้านล่าง
ผู้เชี่ยวชาญของเราจะติดต่อคุณภายใน 6 ชั่วโมงเพื่อหารือเกี่ยวกับความต้องการเครื่องจักรและกระบวนการของคุณ
ข้อผิดพลาด: ไม่พบแบบฟอร์มติดต่อ.