Convert mesh size to microns e microns to mesh across four sieve standards — ASTM E11, Tyler, ISO 565 / BS 410 and JIS Z 8801. Built for mineral processors, chemical and battery-material plants that have to translate an old mesh specification into a real D50 / D97 target for a jet mill or air classifier.
Enter a value and press convert. The tool interpolates geometrically between standard sieve apertures, so it also returns a usable figure for mesh numbers that are not in the published tables.
Full conversion chart for the selected standard. Switch standards to rebuild the table instantly.
| Mesh | Micron (µm) | Millimetre (mm) | Inch | Typical powder application |
|---|---|---|---|---|
| 3 | 6730 | 6.73 | 0.26496 | Crushed mineral, refractory aggregate, ceramic body |
| 3.5 | 5660 | 5.66 | 0.22283 | Crushed mineral, refractory aggregate, ceramic body |
| 4 | 4760 | 4.76 | 0.1874 | Crushed mineral, refractory aggregate, ceramic body |
| 5 | 4000 | 4 | 0.15748 | Crushed mineral, refractory aggregate, ceramic body |
| 6 | 3360 | 3.36 | 0.13228 | Coarse quartz sand, fertiliser granulation feed |
| 7 | 2830 | 2.83 | 0.11142 | Coarse quartz sand, fertiliser granulation feed |
| 8 | 2380 | 2.38 | 0.0937 | Coarse quartz sand, fertiliser granulation feed |
| 10 | 2000 | 2 | 0.07874 | Coarse quartz sand, fertiliser granulation feed |
| 12 | 1680 | 1.68 | 0.06614 | Foundry sand, coarse chemical crystals |
| 14 | 1410 | 1.41 | 0.05551 | Foundry sand, coarse chemical crystals |
| 16 | 1190 | 1.19 | 0.04685 | Foundry sand, coarse chemical crystals |
| 18 | 1000 | 1 | 0.03937 | Foundry sand, coarse chemical crystals |
| 20 | 850 | 0.85 | 0.03346 | Putty powder, dry-mix mortar, detergents |
| 25 | 710 | 0.71 | 0.02795 | Putty powder, dry-mix mortar, detergents |
| 30 | 600 | 0.6 | 0.02362 | Putty powder, dry-mix mortar, detergents |
| 35 | 500 | 0.5 | 0.01969 | Putty powder, dry-mix mortar, detergents |
| 40 | 425 | 0.425 | 0.01673 | Food powder, resin, agricultural chemicals |
| 45 | 355 | 0.355 | 0.01398 | Food powder, resin, agricultural chemicals |
| 50 | 300 | 0.3 | 0.01181 | Food powder, resin, agricultural chemicals |
| 60 | 250 | 0.25 | 0.00984 | Food powder, resin, agricultural chemicals |
| 70 | 212 | 0.212 | 0.00835 | Creatine monohydrate, spices, coarse fillers |
| 80 | 180 | 0.18 | 0.00709 | Creatine monohydrate, spices, coarse fillers |
| Mesh | Micron (µm) | Millimetre (mm) | Inch | Typical powder application |
|---|---|---|---|---|
| 100 | 150 | 0.15 | 0.00591 | Creatine monohydrate, spices, coarse fillers |
| 120 | 125 | 0.125 | 0.00492 | Standard filler grade, cement additive |
| 140 | 106 | 0.106 | 0.00417 | Standard filler grade, cement additive |
| 170 | 90 | 0.09 | 0.00354 | Standard filler grade, cement additive |
| 200 | 75 | 0.075 | 0.00295 | Standard filler grade, cement additive |
| 230 | 63 | 0.063 | 0.00248 | Heavy calcium carbonate, kaolin, ceramic clay |
| 270 | 53 | 0.053 | 0.00209 | Heavy calcium carbonate, kaolin, ceramic clay |
| 325 | 45 | 0.045 | 0.00177 | Heavy calcium carbonate, kaolin, ceramic clay |
| 400 | 37 | 0.037 | 0.00146 | Fine coating grade, glass powder, talc |
| 450 | 32 | 0.032 | 0.00126 | Fine coating grade, glass powder, talc |
| 500 | 25 | 0.025 | 0.00098 | Fine coating grade, glass powder, talc |
| 635 | 20 | 0.02 | 0.00079 | Ultrafine limit of practical sieving |
No woven sieve exists below 635 mesh (20 µm). The mesh numbers below are the nominal trade equivalents still used in quotation across Asia — they are calculated, not measured, so always pair them with a D50 / D97 figure. The convention itself runs out at 12500 mesh (1 µm); below that, only microns and surface area are meaningful.
| Mesh (nom.) | Micron (µm) | Millimetre (mm) | Inch | Typical powder / process |
|---|---|---|---|---|
| 800 | 18 | 0.018 | 0.000709 | Coating-grade GCC, talc, kaolin |
| 1000 | 13 | 0.013 | 0.000512 | Fine coating grade, paint filler |
| 1250 | 10 | 0.01 | 0.000394 | Coating-grade GCC, plastics filler |
| 1500 | 8 | 0.008 | 0.000315 | Ultrafine filler, ink, pigment |
| 2000 | 6.5 | 0.0065 | 0.000256 | Ultrafine filler, battery precursor |
| 2500 | 5.5 | 0.0055 | 0.000217 | Ultrafine, jet mill + classifier |
| 3000 | 5 | 0.005 | 0.000197 | Ultrafine, jet mill + classifier |
| 4000 | 3.4 | 0.0034 | 0.000134 | Sub-micron milling, technical ceramics |
| 5000 | 2.7 | 0.0027 | 0.000106 | Sub-micron, electronic materials |
| 6000 | 2.5 | 0.0025 | 0.0000984 | Sub-micron, high-purity chemicals |
| 8000 | 1.6 | 0.0016 | 0.000063 | Nanomilling territory, pigments |
| 10000 | 1.3 | 0.0013 | 0.0000512 | Nanomilling, pharmaceutical |
| 12500 | 1 | 0.001 | 0.0000394 | Colloidal range, research scale |
A mesh number is a sieve concept. It works from 4 mesh (4.75 mm) down to 635 mesh (20 µm), where two things break down at once: the wire cloth becomes too fragile to weave accurately, and fine particles stop behaving independently because van der Waals forces make them agglomerate. Trade still quotes 1250 or 3000 mesh above that point, but those are nominal equivalents — the table above converts them, and nothing below 20 µm should be accepted as a sieve specification.
That is why modern powder specifications are written as a particle size distribution measured by laser diffraction, not as a mesh count:
A useful rule of thumb: mesh describes the ceiling, D97 describes the guarantee. A “325 mesh” calcium carbonate can have a D50 anywhere between roughly 8 µm and 20 µm depending on how it was classified — and those two products behave completely differently in a coating or a polymer compound.
Use your converted micron value to pick the grinding and classification route. This is the selection logic EPIC process engineers apply during feasibility trials.
| Target fineness | Micron range | Approx. mesh | Recommended EPIC equipment | Typical materials |
|---|---|---|---|---|
| Coarse | 800 – 4750 µm | 4 – 20 | Moinho de rolos, Vibration Mill ZM | Quartz, feldspar, refractory aggregate, ceramic body |
| Medium-fine | 100 – 800 µm | 20 – 140 | Turbo Mill RTM, Moinho Multirotores | Chemicals, food powder, resin, fertiliser, biomass |
| Multar | 45 – 150 µm | 100 – 325 | Pin Mill MJL, Pin Mill PM, Sistema de classificação de moinho de bolas | Heavy calcium carbonate, limestone, putty powder, dry-mix mortar |
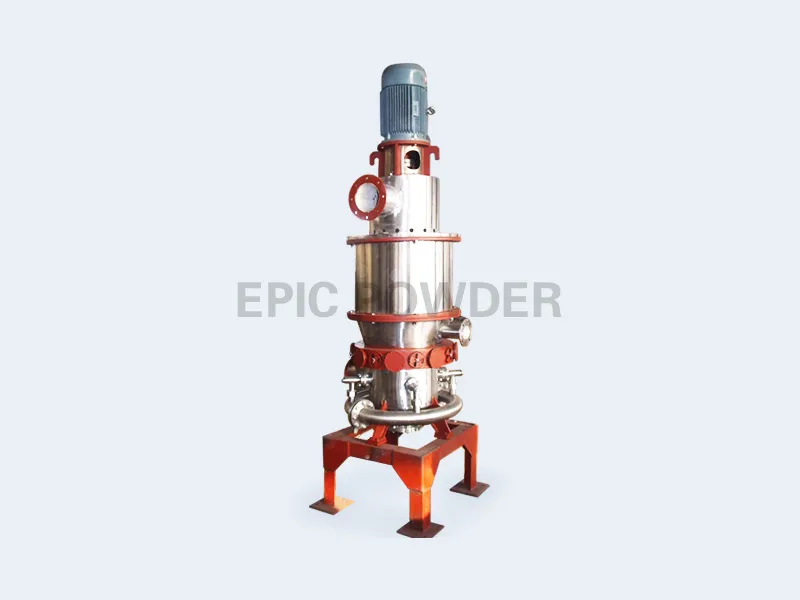
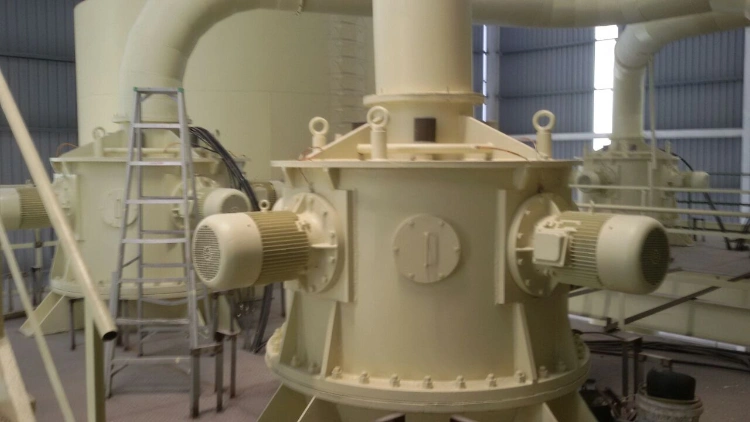
| Ultrafine | 10 – 45 µm | 325 – 1250* | Moinho Classificador de Ar MJW-L, MJW-W, MJW-A | Kaolin, talc, bentonite, ceramic clay, glass powder, creatine |
| Sub-micron to 10 µm | 3 – 10 µm (D97) | Beyond sieve range | Spiral Jet Mill MQP, Fluidized Bed Jet Mill MQW, MQL | Natural & synthetic graphite, cobalt hydroxide, alumina, silica, toner, API |
| Tightest cut | < 3 µm (D97) | Not measurable by sieve | Jet mill + Turbo Double Classifier TDC ou CTC | Battery cathode/anode materials, high-purity ceramics, polishing powder |
* Mesh numbers above 635 are nominal conversions only. Woven wire sieves are not used for routine quality control below 20 µm.
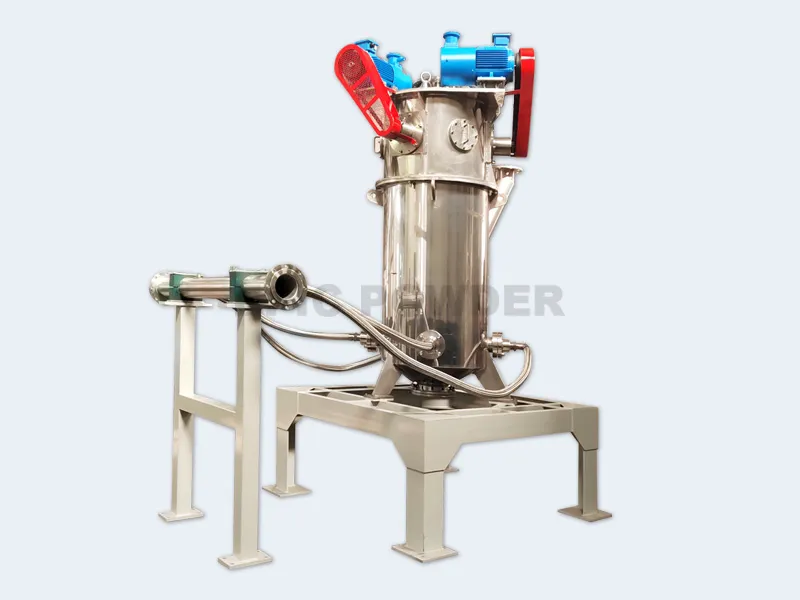
Media-free grinding, D97 from 2 to 45 µm, no iron pickup — the standard route for battery materials and high-purity ceramics.
View jet mill range →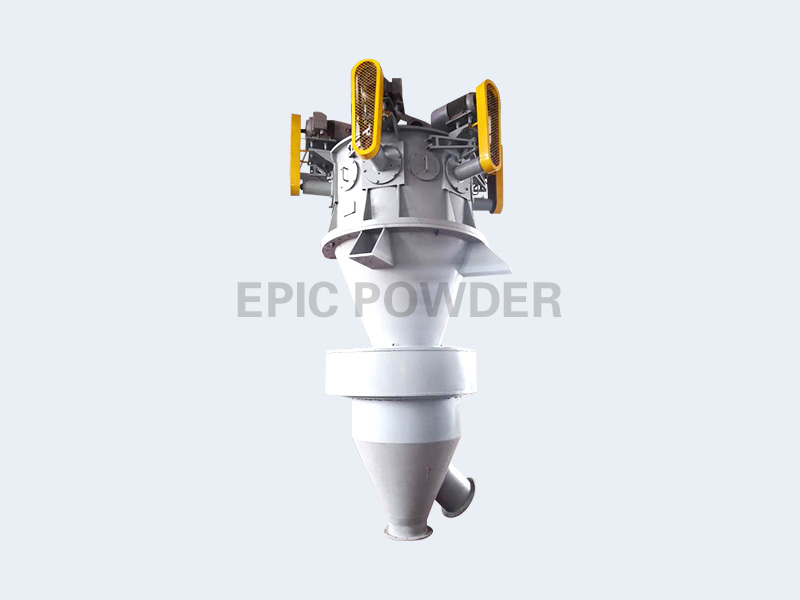
Five classifier families, cut points from 2 to 150 µm, standalone or closed-circuit with any mill.
View classifier range →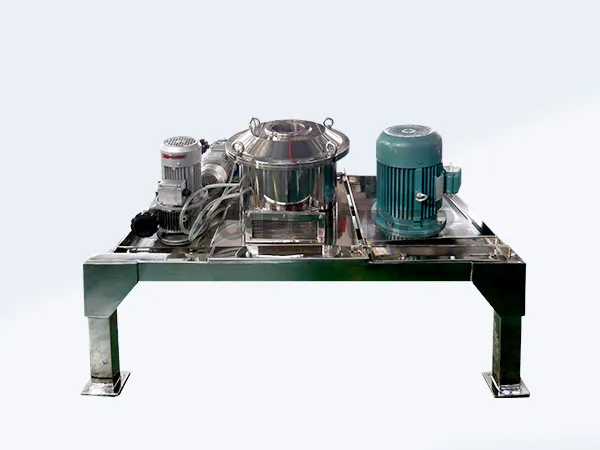
Grinding and classification in one housing for 10–45 µm production, with a far lower energy cost than a jet mill in that band.
View MJW series →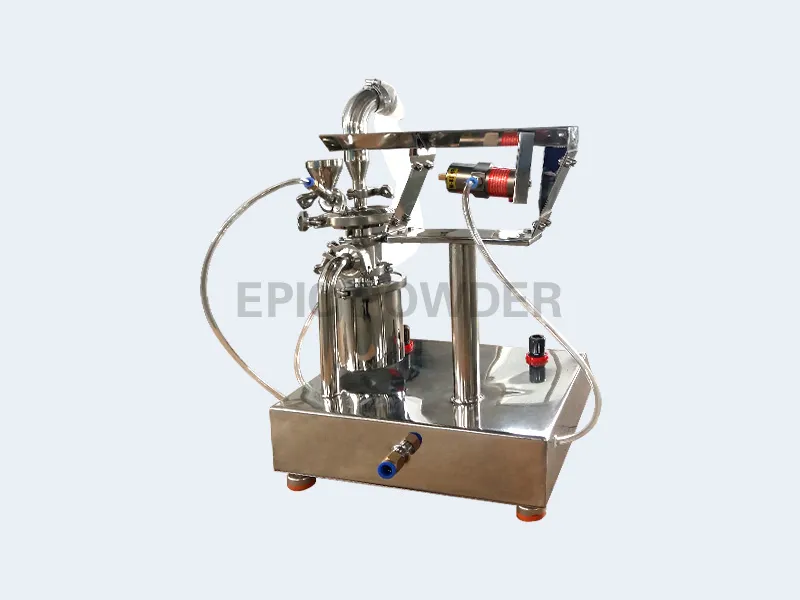
Confirm your D50 / D97 target on 50 g to 5 kg before committing to a production line.
Book a feasibility test →Convert first, then compare against what these materials actually run at in production. Figures below are typical commercial specifications, not limits.
| Material | Typical D50 | Typical D97 | Nearest ASTM mesh (top size) | Route |
|---|---|---|---|---|
| Heavy calcium carbonate (GCC), coating grade | 2.0 µm | 10 µm | ~1250 | Ball mill classifier or pin mill + coating |
| GCC, filler / putty grade | 10 µm | 45 µm | 325 | Pin mill MJL or ball mill classifier system |
| Natural graphite, battery anode | 12 µm | 35 µm | ~400 | Air classifier mill + shaping |
| Synthetic graphite, ultra-fine | 5 µm | 15 µm | ~800 | Jet mill MQW / MQL + HTS classifier |
| Cobalt hydroxide, battery precursor | 4 µm | 12 µm | ~1000 | Fluidized bed jet mill, inert gas option |
| Alumina / aluminium hydroxide filler | 3 µm | 10 µm | ~1250 | Jet mill + high-efficiency classifier |
| Glass powder, electronic grade | 6 µm | 20 µm | ~635 | Mill + HTS air classifier |
| Kaolin / ceramic clay | 8 µm | 45 µm | 325 | Air classifier mill MJW |
| Creatine monohydrate, food grade | 40 µm | 150 µm | 100 | Air jet mill, sanitary design |
| Silica / quartz powder | 7 µm | 25 µm | ~500 | Jet mill, wear-protected lining |
How a D50 of 12 µm with a controlled coarse tail is reached for lithium-ion anode material.
Read the battery material case →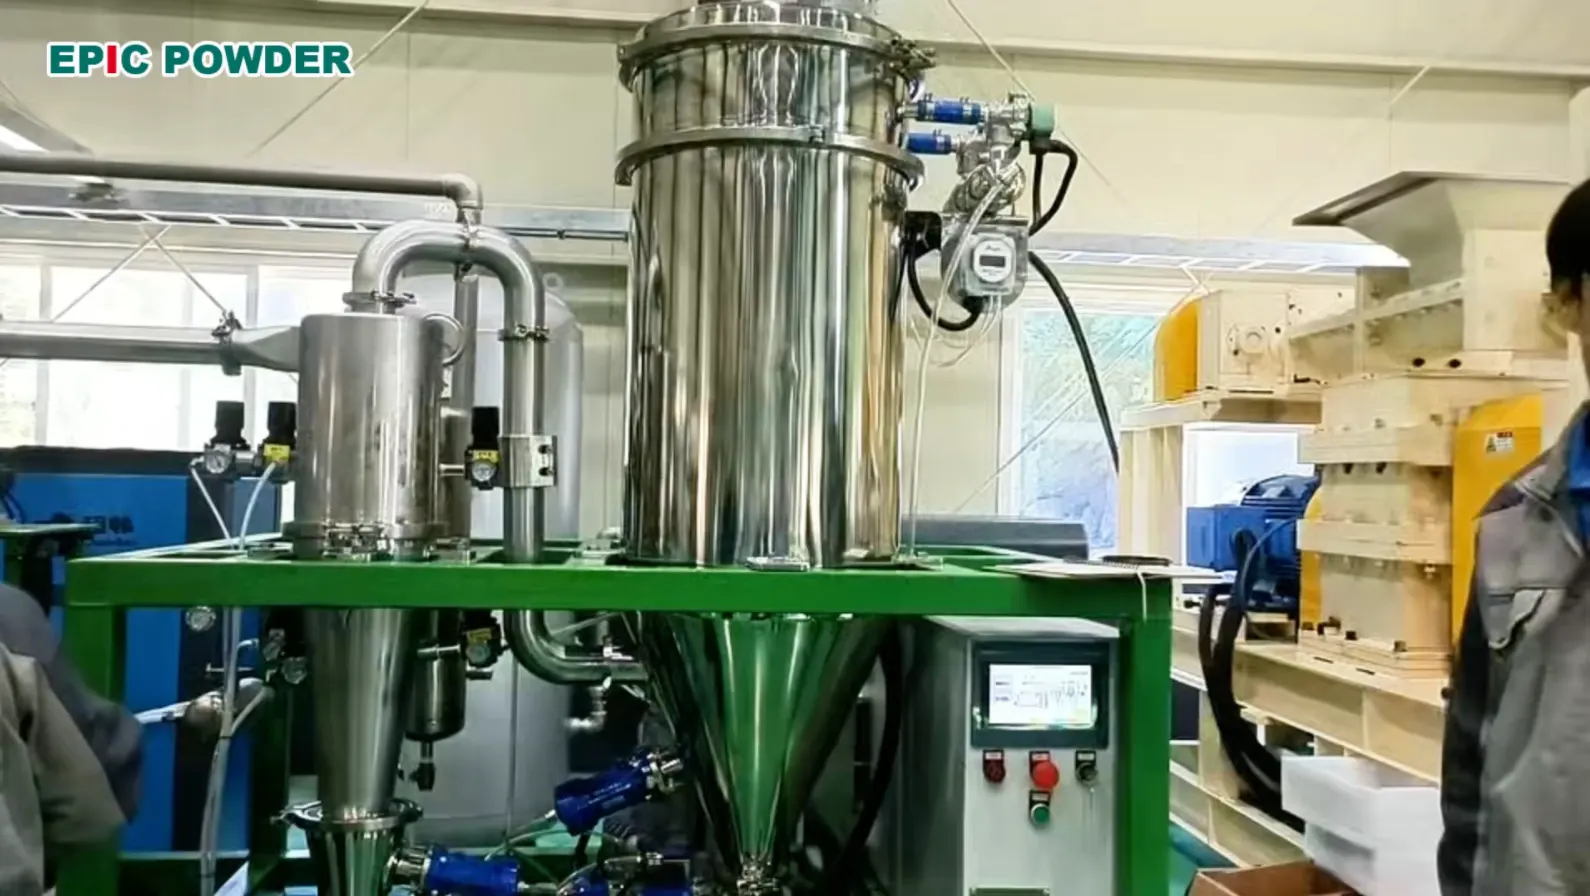
A D97 of 12 µm with no metallic contamination — why media-free grinding is mandatory here.
See the MQL jet mill →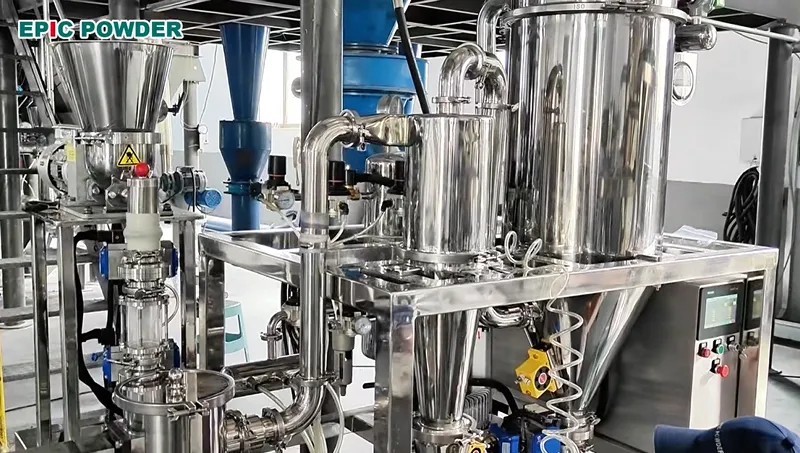
A food-grade application where a 100 mesh specification still works — and where it starts to break down.
Explore jet mills →A mill cannot be sized from a mesh number alone. Two powders with an identical top size can differ by a factor of three in specific energy consumption, depending on hardness, friability, moisture and the shape of the coarse tail. Send this instead:
Once the particle size is right, most filler applications also need a surface treatment. Stearic acid coating on calcium carbonate, for example, is done inline in a continuous coating system immediately after grinding — coating a powder that has already cooled and agglomerated gives a far less uniform result.
This is a fine-powder step, not a coarse one: the feed is normally everything passing 325 mesh (45 µm), production runs from about 1250 mesh (10 µm) down to D97 3 µm, and 95 % activation is the usual acceptance figure. A 45–150 µm powder is too coarse to coat economically — its specific surface is small, so there is little area for the modifier to bond to and the dose per tonne climbs.
EPIC builds four dedicated coating machines for this step: the three-rotor CRM (325–3000 mesh, stearic acid, self-heating), the honeycomb mill MRD (dries filter cake and coats in one pass), the pin mill coating machine PM (highest shear, down to D97 3 µm) and the turbo mill RTM (heat-sensitive and fibrous powders).
Mesh is a count — the number of openings per linear inch in a woven wire sieve. Micron (micrometre, µm) is a length — one millionth of a metre. A higher mesh number means more, smaller openings, so the powder that passes is finer. Because mesh is a count and not a length, the two are not linearly related; you have to convert through a standard sieve table such as ASTM E11.
Under ASTM E11, 200 mesh has a nominal opening of 75 µm. Under the Tyler equivalent it is 74 µm. In ISO 565 / BS 410 the nearest standard aperture is 71 µm or 75 µm depending on the series. Always state which standard a mesh specification refers to.
No. Mesh describes the sieve aperture, not the particle. Material that passes a 325 mesh (45 µm) sieve can be anything from 45 µm down to sub-micron. Sieving only tells you the upper bound of the distribution, which is why modern specifications use D50, D90 and D97 measured by laser diffraction.
D50 is the median: 50 % of the powder volume is finer and 50 % coarser. D90 means 90 % of the volume is finer. D97 means 97 % is finer, and it is the most common guarantee point in ultrafine powder contracts because it controls the coarse tail that causes surface defects, nozzle blocking and inconsistent reactivity.
Below roughly 20 µm, woven wire cloth becomes mechanically fragile and blinds very quickly. Fine particles also agglomerate through van der Waals forces, so they no longer pass independently through the openings. Air classification and laser diffraction replace sieving in this range — a classifier cuts by the balance of centrifugal force and drag, and laser diffraction reports a full distribution rather than a single pass/fail size.
Use whichever standard your customer or your existing specification already names. ASTM E11 dominates North America and most global mineral trade; Tyler is the legacy US system still written into many older plant specifications; ISO 565 and BS 410 are aperture-based and standard across Europe and the UK; JIS Z 8801 is used in Japan. If you want an unambiguous global specification, quote the aperture in microns rather than a mesh number.
Give the material, the target D50 and D97 in microns, the required throughput in kg per hour, and the measurement method. Add the constraints that matter — iron contamination limits, moisture, temperature sensitivity and explosion risk. A single mesh number is not enough for a mill supplier to size equipment.
A fluidised bed or spiral jet mill coupled with a high-efficiency turbo classifier. EPIC builds this around the MQL e MQW fluidised bed jet mills and the MQP spiral jet mill, paired with ITC, HTS, CTC ou TDC classifiers. Jet milling has no grinding media, so it also avoids the iron contamination that disqualifies mechanical mills for battery materials and high-purity ceramics.
Convert your mesh specification to microns, then send us the material and the D50 / D97 you need. EPIC runs feasibility trials on laboratory jet mills and classifiers and returns a measured particle size distribution plus an energy estimate before you commit to a production line.
Request a grinding test Browse powder machineryCalculated values are nominal standard sieve apertures for guidance in process design and quotation. Figures above 635 mesh (below 20 µm) are nominal trade equivalents, not physical apertures — no woven sieve exists there. Woven wire sieves carry a manufacturing tolerance and wear in service, so for contractual or quality-control purposes always verify against calibrated sieves or a laser diffraction analyser. ISO 565 / BS 410 and JIS Z 8801 are aperture-based standards; the mesh figures shown for them are nominal equivalents. Last reviewed October 2026 by EPIC Powder Equipment.