Powder Surface Modifier Dosage Calculator
This modifier dosage calculator answers the question every coating trial starts with: how much stearic acid, silane or titanate does this powder actually need? Enter the material, the modifier and the median particle size, and it returns a figure in percent and kilograms per tonne — with every assumption shown, so you can check it against your own trial data instead of trusting a black box.
How the Modifier Dosage Calculator Works
A coating is a surface phenomenon, so the dose follows the surface rather than the weight. The modifier dosage calculator runs three steps, and you can reproduce every one of them by hand or in a spreadsheet.
SSA = 6 / (ρ × D50) × R
For spheres, in m²/g, with D50 in microns and density ρ in g/cm³. R is a roughness factor: real particles are not smooth spheres, so the geometric value is multiplied up. A 10 µm GCC gives 0.22 m²/g geometrically and roughly 1.3 m²/g by gas adsorption.
Γ = M × 1000 / (Nₐ × a × 10⁻¹⁸)
Grams of modifier needed to cover one square metre once, where M is the molecular weight and a the molecular footprint in nm². For stearic acid (M 284.5, a 0.20 nm²) this comes out at 2.36 mg/m² — a number worth memorising.
W (%) = SSA × Γ / 10 × E
E is the process factor: multiple layers, modifier that stays in the gas phase, and the excess needed to push the activation rate above 95 %. E = 1 is a perfect monolayer, which no production line achieves.
Background reading: BET theory for how specific surface area is measured; PubChem entry for stearic acid for the molecular weight and packing data used above.
The result is an estimate with a stated model, not a lab value. Two powders with the same D50 can differ by a factor of three in measured surface area once you account for internal porosity, which is why the measured-BET mode matters and why every modifier dosage calculation ends with a trial.
Typical Modifier Dosage by Material
Density drives the geometric surface area; the molecular footprint drives how much modifier one square metre accepts. The values below are the ones built into the calculator, and the last column is the range we see on real production lines.
| Matériel | Density (g/cm³) | Roughness R | Typical modifier dosage | Model note |
|---|---|---|---|---|
| Ground calcium carbonate | 2.70 | 6 | 0.6 – 1.5 % | Stearic acid, well behaved |
| Precipitated calcium carbonate | 2.70 | 9 | 1.0 – 3.0 % | Higher area than GCC at the same D50 |
| Talc | 2.75 | 4 | 0.5 – 1.2 % | Platelets, low accessible area |
| Kaolin | 2.60 | 6 | 0.5 – 1.5 % | Silane preferred for paper and rubber |
| Aluminium hydroxide | 2.42 | 6 | 0.8 – 2.0 % | Silane for flame-retardant fillers |
| Magnesium hydroxide | 2.36 | 8 | 1.0 – 2.5 % | Surface area rises sharply when fine |
| sulfate de baryum | 4.50 | 4 | 0.5 – 1.2 % | High density lowers area per gram |
| Fumed silica | 2.20 | — | 3 – 8 % | Hydroxyl-density model, not geometry |
| Precipitated silica | 2.10 | — | 2 – 6 % | Hydroxyl-density model, not geometry |
| Graphite | 2.25 | — | 3 – 8 % | Pitch or resin coating, not a monolayer |
| Modifier | Molecular weight (g/mol) | Footprint (nm²) | Monolayer mass (mg/m²) |
|---|---|---|---|
| Stearic acid | 284.5 | 0.20 | 2.36 |
| Calcium stearate | 606 | 0.35 | 2.88 |
| Silane KH-550 | 221 | 0.30 | 1.22 |
| Silane KH-570 | 248 | 0.32 | 1.29 |
| Titanate coupling agent | 500 | 0.45 | 1.84 |
| Aluminate coupling agent | 350 | 0.40 | 1.45 |
Which Coating Machine Applies This Dosage
A dosage figure only becomes a product when it runs through a machine that can disperse the modifier fast enough to reach the fresh surface. EPIC builds four continuous coating machines, and the modifier dosage calculated above is applied by one of them.
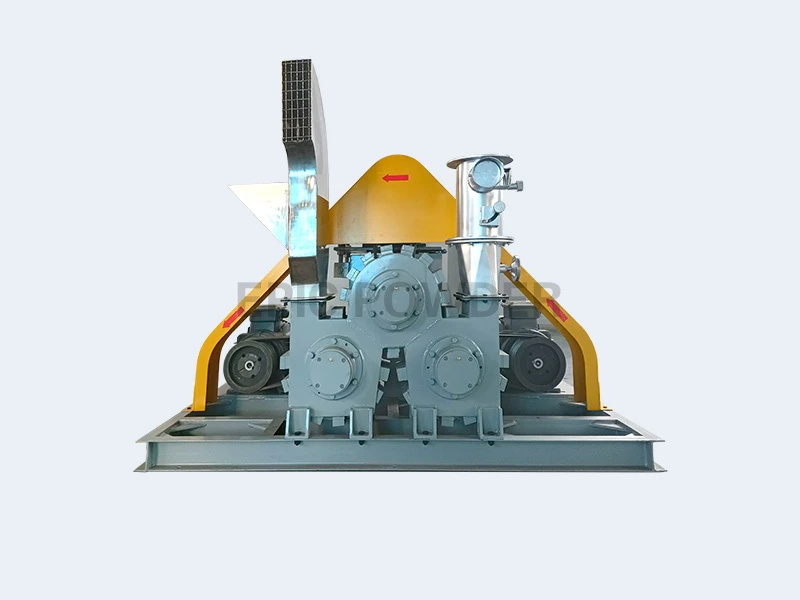
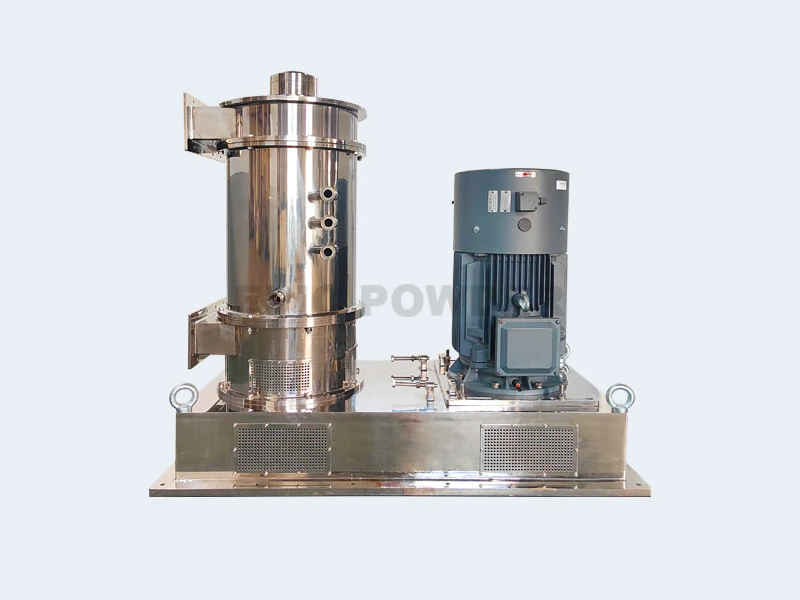
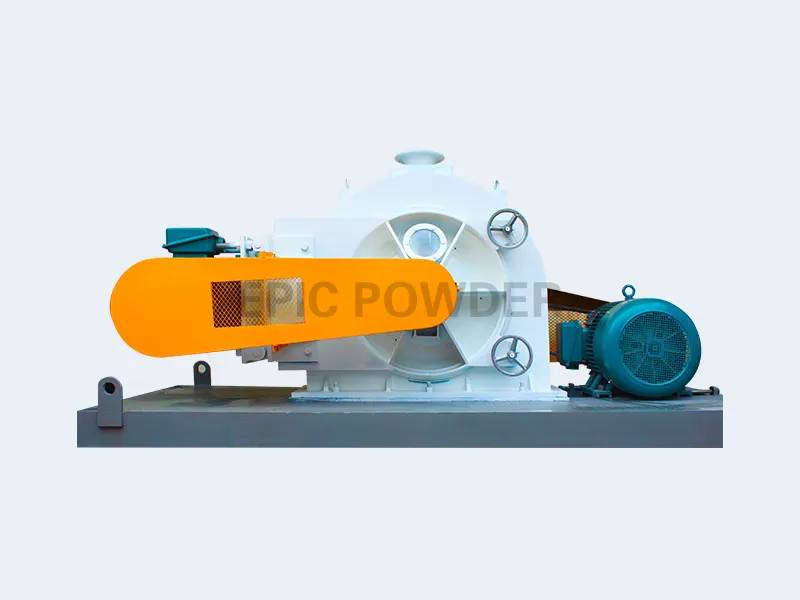
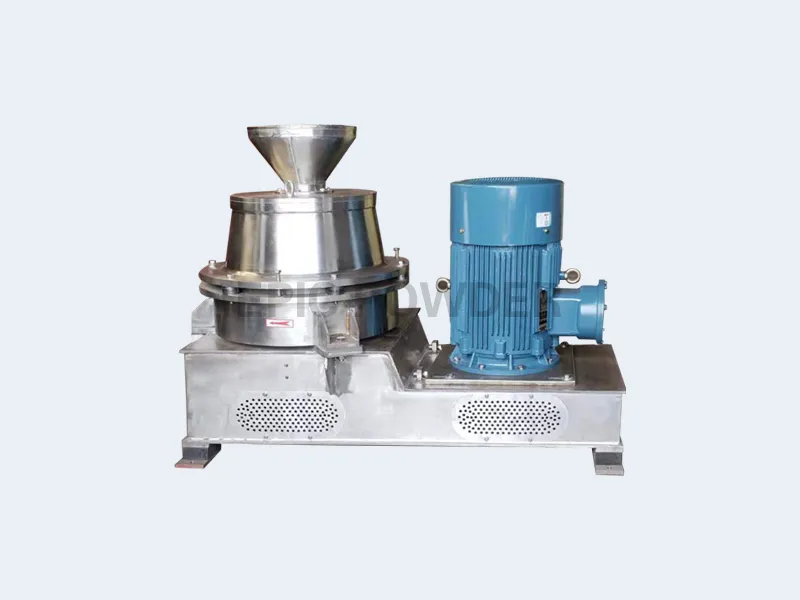
All four run the same upstream sequence: buffer hopper, weighing screw feeder, magnetic separator, melting tank, heated metering pump, coating host, pulse collector, induced-draft fan and PLC cabinet. The continuous coating system overview covers how each machine handles the modifier, and the CRM specification page gives the fineness and capacity table behind the 325–3000 mesh range quoted above.
Where the Modifier Dosage Estimate Breaks Down
Three situations need a trial rather than a number, and the calculator flags all of them.
- Very high surface area — above about 30 m²/g, silane reacts with surface hydroxyls at roughly 2–3 groups per nm², so coverage stops being a geometric question. Fumed and precipitated silica therefore switch to an empirical range.
- Carbon coating — pitch or resin on graphite anode material is a pyrolysis process, not a molecular monolayer, so mass yield has nothing to do with molecular footprint.
- Porous or surface-treated feed — if the powder already carries a dispersant from upstream milling, part of the surface is occupied and the effective dose drops.
In all three cases the output panel shows a warning and an empirical range instead of a calculated figure.
Reading the Result Like a Coating Engineer
Numbers on a screen do not coat powder. These are the four checks our process engineers run before a dosage leaves the trial stage, and each one catches a different failure.
Check 1 — activation rate by float test
Stir a weighed sample into water. The fraction that stays floating is the activation rate, and 95–98 % is the normal acceptance window. Below 90 % the powder still wets out, and dispersion in polymer will suffer no matter what the dosing pump says. The mesh to micron calculator is useful here: if the feed is coarser than you assumed, the surface area — and therefore the dose — is lower than calculated.
Check 2 — oil absorption before and after
Oil absorption value should fall sharply once the surface turns organophilic. If it barely moves while the activation rate looks acceptable, the modifier is present but not bonded — usually because the feed was too cold when it entered the machine.
Check 3 — feed temperature at the injection point
Stearic acid melts at 69 °C. Modifier that has not melted cannot spread, so a cold feed produces a high dosage with a poor result. This is the single most common reason a calculated figure fails in the plant, and the reason three-rotor machines rely on friction heating while pin mill lines often need a pre-heater.
Check 4 — thermogravimetric analysis
TGA is the only check that separates “how much was fed” from “how much is actually on the particle”. Run it when a supplier disputes a result or when a customer changes the downstream specification.
Frequently Asked Questions
Choosing a modifier dosage figure
How much stearic acid does calcium carbonate need?
For ground calcium carbonate, most production lines run between 0.6 % and 1.5 % by weight. At 1250 mesh (about 10 µm) the figure usually lands near 0.8–1.0 %; at 2500 mesh (5 µm) it moves to 1.2 % or slightly more. Precipitated calcium carbonate needs more, because its measured surface area is far higher than its D50 suggests. Running the modifier dosage calculator with a measured BET value is the fastest way to see that difference.
Why is my supplier’s recommended dose higher than the calculated one?
Because the calculation returns a monolayer. A real line needs several times that: modifier partitions into the gas phase, some is lost to the filter, and an activation rate above 95 % usually requires a visible excess. The process factor box handles this — raise it to 2.5–3.0 and the number normally matches what a supplier quotes. If it still does not, ask for the measured surface area of your actual powder; it is usually higher than the geometric estimate.
Does a finer powder always need proportionally more modifier?
Theoretically yes, because surface area scales with 1/D50. In practice the curve flattens at the fine end: agglomerates hide part of the surface from the modifier, and once the activation rate is above 95 % the extra dose mostly goes to waste. That is why the reference ranges narrow rather than widen as you go finer.
Verification and special cases
What activation rate should I target?
95–98 % is the normal acceptance window for mineral fillers, measured by the float test. Below 90 % the powder still wets out in water and dispersion in polymer suffers; above 99 % you are usually paying for modifier that does nothing. If activation is low at the calculated dose, check the feed temperature before increasing the dose — modifier that has not melted cannot coat.
Can I use this calculator for silane on silica?
Only with the warning in mind. Silane does not form a continuous film on silica; it grafts onto surface hydroxyl groups, so the dose follows hydroxyl density rather than geometric area. That is why the calculator switches fumed and precipitated silica to an empirical range and tells you to confirm by trial.
How is the real dosage confirmed in production?
Three checks, in increasing order of effort: the float test for activation rate, oil absorption value before and after coating, and thermogravimetric analysis for the actual organic content. TGA is the only one that tells you how much modifier is really on the particle rather than how much was fed.
Related Equipment and Reading
- Continuous coating systems — the four machines this dosing applies to
- Three-rotor coating machine (CRM)
- Pin mill coating machine (PM)
- Mesh to micron calculator — get D50 before you dose
- How to choose a surface modifier
- Stearic acid coating of GCC, step by step
- Five common modifiers for calcium carbonate
- Mineral filler applications
Send the Powder. We Will Return a Measured Dosage.
A modifier dosage calculator gets you into the right range. A trial tells you the real number: send 5–10 kg with your target activation rate and application, and we return the coated sample, the activation curve and the recommended machine setting.
Request a coating trial See the coating systems